If you’ve ever stood in a plant control room watching a process line veer off course because a valve didn’t open or close when it was supposed to, you know how much a small component like a valve positioner matters. As a valve positioner supplier, I’ve seen first-hand how even the most reliable, precision-built positioner will fail to do its job if it’s not installed correctly. I’ve worked with plant maintenance teams, instrument technicians, and project engineers over the last 12 years, and the one mistake I see most often is skipping or cutting corners on installation requirements, thinking it’s just “bolting a box onto a valve.” It’s not. It’s a system that relies on alignment, air supply, signal integrity, and environmental factors to work as intended, and getting any of these wrong leads to errors, downtime, and unnecessary repair costs. Today, I want to walk through the actual installation requirements we share with every customer when they order our positioners, the ones we’ve learned from hundreds of site visits and troubleshooting calls, not just the generic specs in a manual. Valve Positioner

Physical Mounting: The Foundation of Reliability
The first, and most critical, step in installation is getting the positioner mounted correctly to the valve actuator. This isn’t just tightening two bolts. Let’s start with alignment. The positioner’s feedback mechanism—the arm or linkage that connects it to the actuator’s stem—has to be perfectly aligned with the stem’s axis. If it’s even a few degrees off, the feedback signal will be distorted. I had a customer in a chemical plant a few years back that mounted a positioner 15 degrees off center, and for three months, their control system was reading a 5% error in flow rates they couldn’t explain. When we sent a technician out, it took 20 minutes to loosen the mounting bracket, adjust the arm, and re-align it. The error was gone instantly.
The mounting surface also matters. You can’t mount a positioner to a soft steel valve body or a thin actuator bracket that flexes when the valve operates. Flex in the mount means the feedback arm moves when it shouldn’t, leading to oscillation or “chatter” in the valve. We always recommend using a rigid, vibration-damped mounting bracket, especially for applications that involve high process pressures or frequent valve cycling. For example, in a steam line that cycles dozens of times an hour, a flimsy mount will wear out in months, not years. Also, the positioner needs to be mounted at a height that’s accessible for maintenance, but not so low that it’s exposed to process drips, debris, or water pooling. We usually suggest 3 to 5 feet above the floor or platform, or as specified in the valve’s OEM documentation.
Another physical mounting detail: the weight of the positioner itself. Most of our industrial positioners weigh between 10 and 25 pounds. If you’re mounting it to a large, heavy-duty actuator, the weight might not be an issue, but for small, quarter-turn actuators on butterfly or ball valves, mounting the positioner can throw off the actuator’s balance. That’s why we offer lightweight, compact positioner models for small actuators, and we always provide load calculations for every application to make sure the mount doesn’t stress the actuator shaft.
Pneumatic Air Supply: The Lifeblood of the Positioner
Valve positioners are pneumatically operated, for the most part, so they need a consistent, clean, dry air supply. This is another area where I see customers cut corners, and it almost always causes problems. The minimum air pressure requirement is usually between 20 and 100 psi, depending on the positioner model and the actuator size. But the key isn’t just pressure—it’s pressure stability. If the air supply fluctuates by more than 5%, the positioner can’t hold a steady signal, leading to valve drift. For example, in a pulp and paper mill where the valve controls the flow of black liquor, even a small amount of drift can throw off the entire recovery process.
Cleanliness is even more important. Compressed air from plant lines often has oil, water, and particulate matter in it, especially if the plant’s air dryers or filters are poorly maintained. A positioner’s nozzle and flapper mechanism, or its electronic control components, can get clogged with even 10 microns of debris. That’s why we always mandate a properly sized filter regulator and lubricator (FRL) as part of the installation. The FRL should be mounted as close to the positioner as possible, usually within 6 inches, to prevent condensation from forming in the air line before it reaches the positioner. The filter should be a 5-micron rated coalescing filter, and the regulator should have a precision adjustment to maintain a constant output pressure to the positioner. We also recommend a water trap drained daily, especially in humid environments. I once had a customer in the Gulf Coast region skip the FRL, and within two weeks, water had flooded the positioner, shorting out the electronics and requiring a full replacement. The cost of the FRL was $150; the cost of the downtime was over $100,000.
Signal Integrity: Making Sure the Control System Talks to the Positioner
Most modern positioners are either 4-20 mA analog or digital (like Hart or Foundation Fieldbus), and both require a clean, uninterrupted signal from the control system. For analog signals, the biggest issue is electrical noise from power lines, motors, or variable frequency drives (VFDs). If the signal wire is run parallel to a 480V power line in a conduit, the noise can cause the positioner to misinterpret the 4-20 mA signal, leading to valve errors. The rule of thumb we give is to separate signal wires from power wires by at least 12 inches, or use shielded twisted-pair cable for analog signals. The shield should be grounded at only one end of the cable to prevent ground loops, which are another common source of noise.
For digital positioners, the requirements are a bit different, but just as strict. Digital signals are more susceptible to signal loss over long distances. We recommend using cable rated for the specific fieldbus protocol, and limiting cable runs to 1,000 feet or less, unless you use a signal repeater. Also, digital positioners often require proper termination at both ends of the cable; forgetting to terminate a Hart signal can cause the control system to lose communication with the positioner entirely, making it impossible to adjust the valve remotely. We always provide a signal wiring diagram with every positioner, and our support team will walk a technician through the wiring over the phone if they have questions—no job is too small, in our book.
Another signal detail: the electrical load of the positioner. For analog positioners, the control system needs to have a loop impedance that matches the positioner’s requirements. If the loop impedance is too high, the 4-20 mA signal will be distorted, especially at the lower end of the range (0-4 mA). We test every positioner before it leaves our warehouse, so when a customer orders, we provide the exact loop impedance requirement for their model, so the control system engineer can size it correctly.
Environmental Considerations: Protecting the Positioner from Its Surroundings
Valve positioners are installed in all kinds of environments, from freezing arctic tanks to hot refinery towers. They need to be rated for the operating temperature and humidity of their location. Our standard positioner models are rated for -40°F to 185°F, but for extreme environments—like a furnace exhaust line that runs at 250°F—we offer high-temperature enclosures or heat exchangers to keep the positioner’s internal components within their safe operating range.
Humidity is another factor. If the positioner is installed in a coastal refinery or a wastewater plant where humidity is over 90%, we recommend a NEMA 4X rated enclosure, which is water-tight and corrosion-resistant. The internal electronics can corrode in high humidity, leading to short circuits or signal errors. We also install desiccant breathers in the enclosure for applications in very humid or dusty environments, to keep moisture out without trapping it inside.
Then there’s vibration. Industrial plants have a lot of it—from pumps, compressors, and large motors. Excessive vibration can loosen the mounting bolts, damage the feedback linkage, or wear out internal components over time. We always recommend checking the vibration level at the installation site before mounting the positioner. If the vibration is over 0.5 g at 10-2000 Hz, we offer vibration-dampening kits that isolate the positioner from the actuator or valve. For example, a customer in a natural gas processing plant had a reciprocating compressor that created high vibration, and their first positioner failed in 6 months due to linkage wear. After we installed our dampening kit, the positioner has been running flawlessly for over 3 years.
Testing and Calibration: The Final Step No One Should Skip
Even if you follow every installation requirement, you need to test and calibrate the positioner before putting it into service. Calibration is adjusting the zero and span of the positioner so that when the control system sends a 4 mA signal, the valve is fully closed, and a 20 mA signal is fully open. Most new positioners come pre-calibrated from the factory, but site conditions—like air pressure, linkage alignment, or the valve’s dead band—can throw off that calibration. We always recommend a site calibration, using either a manual calibrator or the positioner’s built-in diagnostic tool.
Testing is equally important. You should run a full stroke test, sending signals from 0 to 100% and back, to make sure the valve moves smoothly without sticking or jumping. You should also test for drift, holding a mid-range signal for 15 minutes and checking if the valve position changes. If drift is more than 1%, there’s probably an issue with the air supply, signal, or alignment. We include a pre-startup test checklist with every positioner, and our service team can come on site to do the testing for customers that don’t have a dedicated instrument technician.
A Note from Our Experience
Over the years, I’ve seen too many plants lose production hours, thousands of dollars in material, and even safety incidents because of bad positioner installation. It’s not that the positioner is a bad product—it’s that the basic requirements were overlooked. At our company, we don’t just sell positioners; we provide installation guidance, support, and post-sales service because we know that a positioner only works if it’s installed right.
If you’re working on a project, troubleshooting a misbehaving valve, or ordering positioners for your plant, don’t cut corners on installation. Follow the physical, air supply, signal, and environmental requirements we’ve outlined, and reach out to our team for any questions or support. We’re here to make sure your valves work as reliably as they should.
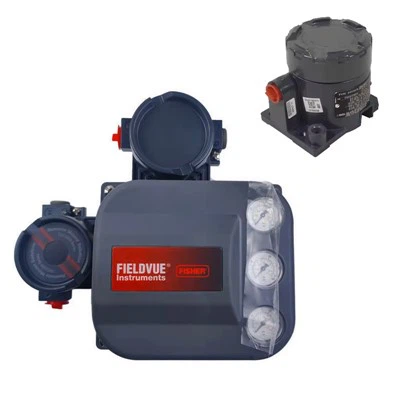
When you’re ready to discuss your specific application, connect with our team to find the right positioner for your needs and walk through the installation details step by step.
References
Valve Accessories Valve Actuator and Positioner Installation, Instrumentation, and Control. ISA-TR75.06.01-2015.
Control Valve Positioner General Installation Guidelines. Emerson Automation Solutions.
Pneumatic Compressed Air Quality Standard. ISO 8573-1:2010.
Century Weiye (Dalian) Control Equipment Co., Ltd.
As one of the leading valve positioner manufacturers and suppliers in China, we warmly welcome you to buy discount valve positioner in stock here from our factory. If you have any enquiry about quotation, please feel free to email us. Quality products and reasonable price are available.
Address: 2205, Building 8, Red Star International, Ganjingzi District, Dalian City, Liaoning Province
E-mail: serena@valvesjwy.com
WebSite: https://www.valve-sjwy.com/
